NEWS
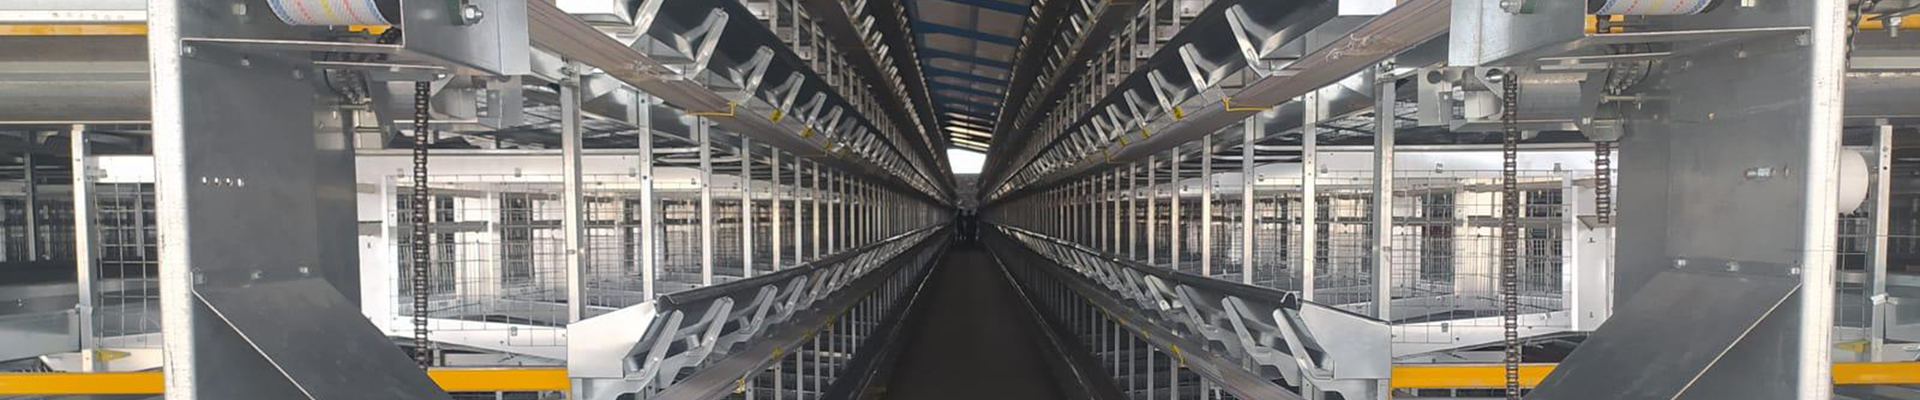
Battery cage selection determines layer-house capacity, automation compatibility, installation planning, and long-term equipment coordination across commercial poultry projects.
Standard battery cage configurations simplify procurement, while custom battery cage engineering adapts equipment around building dimensions and structural restrictions.
Automatic layer cage systems connect feeding, drinking, manure removal, egg collection, and electrical control into coordinated production lines.
Material specifications, conveyor routing, service access, and commissioning parameters directly influence practical battery cage operation across different farm scales.
- Engineering-based battery cage selection combines production targets, house geometry, automation requirements, and expansion planning into one equipment purchasing decision.
Get professional poultry farm construction guidance, equipment selection solutions, and the latest price lists, whatsApp to +8618830120193, click to learn more.
Standard Battery Cage: A Defined Engineering Package
A standard battery cage is manufactured from repeatable modules, enabling production drawings, fabrication jigs, fastener schedules, and installation packages to remain consistent between projects.
For conventional layer houses, battery cage production can therefore move directly from approved drawings into fabrication without redesigning every structural connection.
A commercial battery cage package can also combine cage frames with feed delivery, nipple drinking, egg transfer, manure handling, and control equipment, reducing interface problems between separately sourced machines.
Published commercial systems commonly use cage modules around 1,950 mm in length, with galvanized steel construction and integrated automatic or semi-automatic equipment options.
Data is for reference only.Swipe horizontally to view full table.
Custom Battery Cage: Design From The Building Outward
Custom battery cage engineering begins with the building survey because structural geometry controls equipment positioning, access routes, and conveyor interfaces.
For an existing poultry house, a 100 mm shift in a structural obstruction can change the available cage-row arrangement and require corresponding adjustments to feed and egg-transfer routing.
Our battery cage engineering process can therefore use architectural drawings, site measurements, and equipment centerlines before fabrication, allowing structural conflicts to be identified while changes are still digital rather than on site.
Custom design is particularly useful when an existing building must retain doors, columns, drainage channels, or ventilation openings without relocating major civil structures.
Data is for reference only.Swipe horizontally to view full table.
Standard Vs Custom: Structural Configuration
The engineering distinction between standard and custom battery cage systems is the degree of control over module relationships, not merely the physical cage shape.
A standardized battery cage can repeat the same frame, door, mesh, feeder interface, and connection sequence across multiple houses, making procurement and spare-parts identification easier.
Custom battery cage engineering instead modifies the arrangement where the building or production plan requires a different equipment relationship.
For example, published layer-housing systems can extend individual cage rows to approximately 60–100 m, meaning conveyor routing and drive positioning become important during long-row planning.
Data is for reference only.Swipe horizontally to view full table.
Capacity Calculation: Start With Production Targets
Capacity planning should translate the target flock into physical cage modules, feed distribution routes, drinking points, manure paths, and egg-transfer interfaces.
For a 30,000-layer project, the equipment schedule should be generated before procurement so cage quantity, house layout, and automation interfaces are calculated from one coordinated model.
Our battery cage engineering process can map each production zone to its corresponding equipment circuit, preventing a situation where cage installation is completed before the required feeding or egg-transfer route has been resolved.
Feed demand is another useful design checkpoint: a commercial layer may consume roughly 110 g of feed per day, making daily feed logistics a significant part of equipment planning.
Data is for reference only.Swipe horizontally to view full table.
Building Constraints: Where Custom Engineering Creates Value
The building survey should identify every fixed obstruction before the battery cage layout is released for manufacturing.
Columns, drainage channels, doors, air inlets, exhaust equipment, electrical cabinets, and feed-entry points can all become coordination constraints when cage rows are installed at full length.
Our customized battery cage workflow therefore uses building measurement, equipment layout, and installation simulation as sequential engineering checkpoints.
For a large project, digital layout verification can also determine whether conveyors, service passages, and access doors remain usable after all cage tiers are installed.
A useful design check is to compare the planned cage-row arrangement against the actual structural grid before issuing the production drawing.
Data is for reference only.Swipe horizontally to view full table.
Automation Compatibility: Build One Production Line
A battery cage should be engineered together with its automation because separate equipment purchases can create mismatched drive positions, conveyor elevations, and electrical interfaces.
Feeding, drinking, manure removal, and egg collection each have different operating requirements, so the cage layout must establish common reference points before equipment installation.
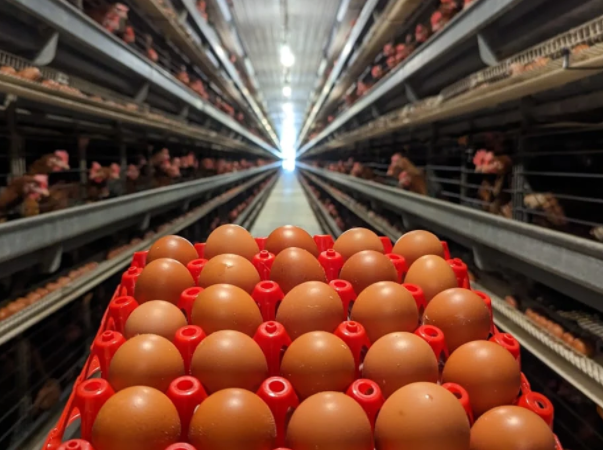
For long commercial systems, central egg handling can reach approximately 65,000 eggs per hour in published equipment configurations, making transfer capacity an engineering issue rather than merely a labor-saving feature.
Our battery cage quotations therefore match automation components to the actual house arrangement, conveyor length, production volume, and control architecture.
Data is for reference only.Swipe horizontally to view full table.
Material Selection: Corrosion Resistance Starts With The Steel
Battery cage structures operate in an environment where moisture and manure-derived gases can accelerate metal degradation, making surface treatment a procurement specification rather than a cosmetic option.
Hot-dip galvanized steel is widely used for commercial layer cages, while some current systems combine galvanized frames with aluminum-zinc coated mesh for additional surface protection.
Our battery cage material selection can therefore be matched to structural loads, cleaning practices, humidity, and expected operating conditions instead of using one material specification for every project.
For long-term maintenance, consistent wire forming and stable frame connections are equally important because damaged or distorted sections can interfere with cage doors, feed troughs, and egg movement.
Data is for reference only.Swipe horizontally to view full table.
Cost Analysis: Evaluate The Complete Equipment System
Battery cage investment should be evaluated from the equipment architecture rather than from the cage frame alone.
Separately purchased cages, conveyors, manure systems, and electrical controls can introduce additional engineering interfaces, installation work, and commissioning responsibilities.
Our commercial battery cage quotation can separate structural equipment from automation and project services, allowing customers to identify exactly which functions are included in the delivered system.
For projects using automated egg handling, published commercial systems demonstrate capacities reaching 65,000 eggs per hour, so conveyor selection should be matched to actual production throughput rather than selected only by purchase price.
Data is for reference only.Swipe horizontally to view full table.
Maintenance Engineering: Design For The Service Team
Maintenance access should be resolved during battery cage design because components hidden behind permanent structures become more expensive to service after commissioning.
Motors, bearings, sensors, water regulators, drive assemblies, and conveyor connections should have identifiable access points and replacement procedures.
A practical maintenance program can combine daily visual checks with scheduled mechanical inspections, allowing abnormal belt tracking, loose fasteners, water leakage, and motor noise to be identified before production is interrupted.
Published battery cage equipment can include manufacturer warranties of approximately one year, while replacement planning should continue beyond the warranty period through standardized component identification.
For customized projects, we therefore recommend standardizing replaceable components wherever possible while reserving customization for the layout itself.
Data is for reference only.Swipe horizontally to view full table.
Installation Workflow: From Drawing To Production
Battery cage installation should proceed from an approved engineering drawing rather than from component packages alone.
The controlled sequence is drawing approval, material preparation, fabrication, shipment, frame positioning, cage assembly, automation installation, electrical connection, and commissioning.
Mechanical commissioning checks structural alignment and moving components first, followed by electrical testing of motors, sensors, control circuits, and safety devices.
For automated battery cage projects, a structured commissioning checklist can contain 20–40 verification points, depending on the number of equipment subsystems and control functions.
This approach converts installation from an assembly task into a documented equipment acceptance process.
Data is for reference only.Swipe horizontally to view full table.
Selection Method: Five Engineering Questions
The battery cage selection process should start with measurable project conditions rather than a generic standard-versus-custom comparison.
Building envelope: can the proposed battery cage arrangement fit the actual structural grid without relocating fixed building elements?
Flock capacity: can the selected cage configuration accommodate the target population while maintaining compatible feed, water, manure, and egg-handling routes?
Automation scope: are feeding, drinking, manure removal, and egg collection being designed as connected systems rather than isolated purchases?
Maintenance access: can operators reach motors, belts, sensors, water components, and electrical equipment after the battery cage is fully assembled?
Expansion plan: can future houses use compatible equipment drawings, components, control architecture, and maintenance procedures?
For a new poultry house with conventional geometry, a standardized battery cage package can reduce design iterations.
For an existing house with structural restrictions, customized row planning can preserve the building while adapting the equipment arrangement.
Data is for reference only.Swipe horizontally to view full table.
Why Choose A Complete Layer Poultry Equipment Supplier?
A commercial battery cage project becomes easier to control when the cage structure and supporting equipment originate from one coordinated engineering package.
Our battery cage solutions can integrate structural cages with feeding, drinking, manure removal, egg collection, environmental interfaces, and electrical controls, creating a single equipment architecture for commercial layer production.
For a 10,000-layer project, our engineering team can calculate cage requirements and then coordinate the associated feeding, watering, manure, and egg-collection equipment around the selected layout.
For multi-house developments, the same battery cage engineering framework can be applied across several buildings so equipment drawings, component identification, and operating procedures remain consistent.
The commercial value comes from reducing interface gaps between separate equipment suppliers while keeping technical specifications visible during quotation, manufacturing, installation, and commissioning.
Our battery cage projects can therefore be supplied as standard configurations or adapted through project-specific engineering when building geometry, production capacity, or automation routing requires modification.
Standard battery cage: appropriate when building geometry and production requirements align with an established equipment configuration.
Custom battery cage: appropriate when structural conditions or automation routing require engineering changes to the equipment arrangement.
Complete poultry equipment solution: appropriate when battery cage, feeding, drinking, manure removal, egg collection, and control systems need coordinated project execution.
Send your poultry-house length, width, height, target layer population, and preferred automation level to our engineering team.
We can then prepare a battery cage layout and equipment configuration based on your actual farm conditions.
Frequently Asked Questions
Q1: What is the difference between a standard battery cage and a custom battery cage?
A1: A standard battery cage follows established modules, while a custom battery cage modifies the equipment arrangement around building geometry, production targets, and automation interfaces.
Q2: Can a battery cage system include automatic feeding and egg collection?
A2: Yes.Commercial battery cage systems can integrate automatic feeding, nipple drinking, manure handling, and egg collection, with published equipment configurations supporting automated central egg handling.
Q3: How should a farm determine the correct battery cage configuration?
A3: The battery cage configuration should be calculated from building dimensions, target flock population, structural arrangement, equipment routing, maintenance access, and planned automation.
A commercial project should complete the layout calculation before cage manufacturing begins.
Taiyu (HK) Group - One Of China Largest Battery Cage Exporter
Battery cage systems combine galvanized structural modules with automated feeding, drinking, manure, and egg-collection equipment, with configurations engineered for multi-tier commercial layer production.
Global factory-direct supply covers battery cage, poultry equipment, automated feeding, drinking, manure removal, egg collection, electrical control, installation guidance, and spare-parts coordination.
Turn-key poultry equipment engineering connects building drawings, battery cage layouts, automation routing, electrical specifications, installation procedures, commissioning checks, and production handover.
Project-based manufacturing supports complete poultry equipment packages for new farms, existing-house upgrades, multi-house developments, and internationally shipped commercial layer facilities.
Engineering documentation includes equipment layouts, technical specifications, component schedules, installation drawings, commissioning procedures, and after-sales technical coordination for battery cage projects.
Contact Us To Received Your Customized Poultry Farm Plan
Headquarters And Branchs
Hong Kong Headquarter Management Team
Hong Kong Headquarter Taiyu Industrial Group CO., LTD
China Hebei Best Machinery And Equipment CO., LTD
Nigeria Vanke Machinery And Equipment CO., LTD
Tanzania Best Machinery And Equipment CO., LTD
Ethiopia Best Hebei Machinery Manufacturing PLC
Reception /24 WhatsApp NO. : +8618830120193
PRODUCTS RECOMMENDED
 China Branch Manufacture Poultry Farm EquipmentRead More
 Ethiopia Branch Manufacture Poultry Farm EquipmentRead More
 Nigeria Branch Manufacture Poultry Farm EquipmentRead More
 Tanzania Branch Manufacture Poultry Farm EquipmentRead More
 IoT Smart Poultry FarmRead More
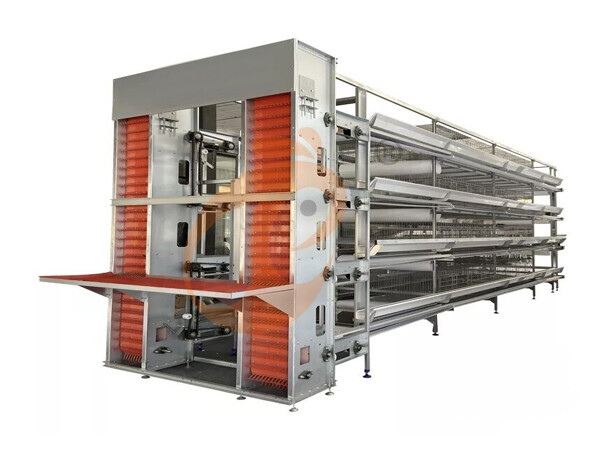
 >30,000 Layers Automatic H Type Battery CageRead More
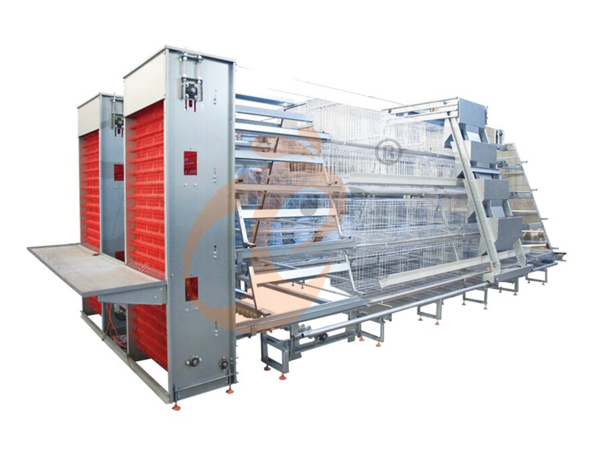
 10,000 - 30,000 Layers Automatic A Type Battery CageRead More
MESSAGE
NEWS
 50,000 - 100,000 chickens/house: poultry farm solution, chicken cage, poultry farm equipment, AI smart managementRead More
 30,000 - 50,000 chickens/house: poultry farm solution, chicken cage, poultry farm equipment, AI smart managementRead More
 10,000 - 30,000 chickens/house: poultry farm solution, chicken cage, poultry farm equipment, AI smart managementRead More
 100 - 10,000 chickens/house: poultry farm solution, chicken cage, poultry farm equipment, AI smart managementRead More