NEWS
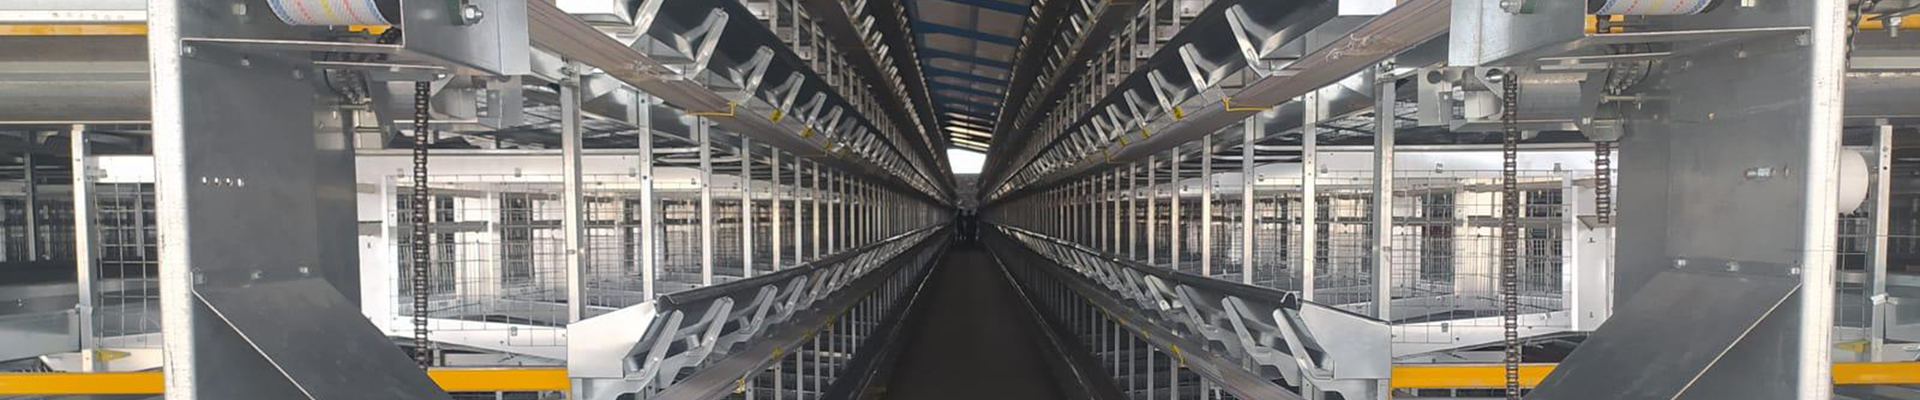
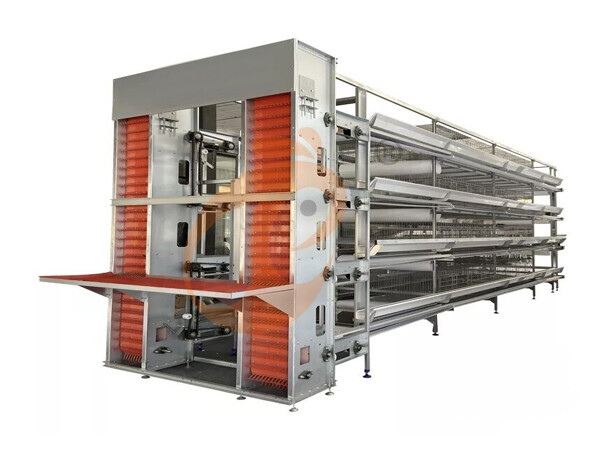
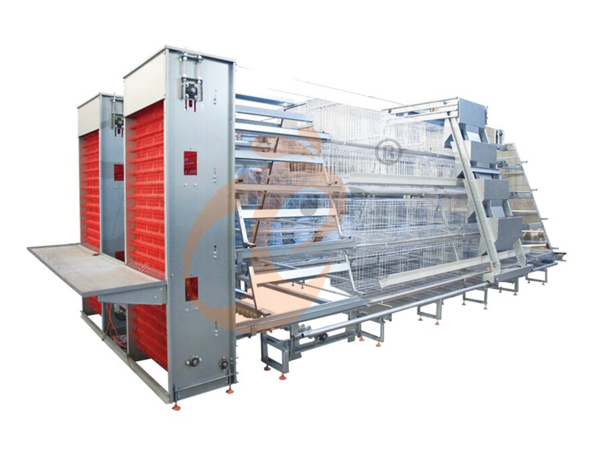
A type battery cage supports layer production through housing, feeding, drinking, egg handling, and manure transfer, with four-tier configurations supporting capacity.
Layer battery cage system economics connect bird capacity, building footprint, labor input, feed management, egg quality, and equipment integration beyond purchase price.
Automatic layer cage system design links plc control, conveyors, ventilation, lighting, and monitoring for consistent workflow.
Cage-free systems add floor, nest, perch, and litter requirements, changing capital allocation, management procedures, and space utilization.
- Equipment selection follows requirements, building dimensions, flock targets, automation levels, and conditions, making engineered configuration central to layer-farm economics.
Get professional poultry farm construction guidance, equipment selection solutions, and the latest price lists, whatsApp to +8618830120193, click to learn more:
Profitability Starts With System Engineering
Engineering focus
A type battery cage profitability is closely connected to housing engineering, with 3–4 production tiers and integrated feeding, drinking, egg collection, manure removal, and environmental control.
Cage-free production follows a different engineering route, requiring coordinated floor, nest, perch, litter, ventilation, and egg-management systems.
Therefore, A type battery cage projects should be evaluated by productive capacity, labor input, building utilization, and market requirements rather than equipment price alone.
A Type Battery Cage: Core Technical Configuration
Data is for reference only.Swipe horizontally to view full table.
A type battery cage uses a trapezoidal frame for compact production equipment, while a layer battery cage system can arrange feeding and drinking components around defined production rows.
Published equipment configurations show cage modules around 1.95 m, while galvanized structures can support long-term commercial operation.
Production Capacity And Building Utilization
Capacity logic
A type battery cage uses vertical building volume to increase productive capacity without requiring equivalent floor expansion.
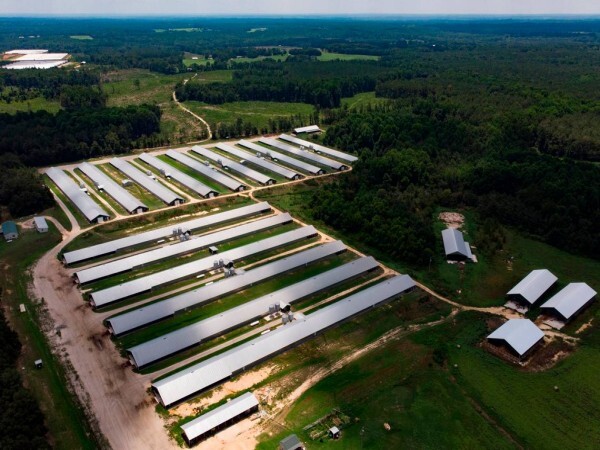
A commercial reference design accommodates 20,160 birds in a 95 × 13 × 4 m house, illustrating how an automatic layer cage system can connect equipment layout with production capacity.
For investors, engineering targets should include birds per building, birds per production line, and eggs delivered to the collection room.
Capacity And Layout Comparison
Data is for reference only.Swipe horizontally to view full table.
Cage-free systems require additional functional zones for movement and management, while A type battery cage production organizes operations through dedicated cage modules and service corridors.
Feeding, Drinking, And Labor Engineering
Workflow sequence
- Feed distribution: A type battery cage uses automatic chain or hopper systems for controlled feed movement.
- Water delivery: A layer battery cage system integrates nipple lines for consistent water access.
- Operator control: An automatic layer cage system connects motors, regulators, and control cabinets into standardized daily procedures.
Published A type configurations use nipple flow around 60–90 ml/min, while feed-line suspension intervals can reach approximately 2–3 m.
Feeding And Drinking Equipment Parameters
Data is for reference only.Swipe horizontally to view full table.
Correct feed and water engineering supports stable A type battery cage operation, while centralized controls can connect meters, regulators, motors, and alarm functions.
Egg Collection And Egg Quality Control
Engineering note: A type battery cage can transfer eggs directly toward collection equipment, reducing repeated manual handling.
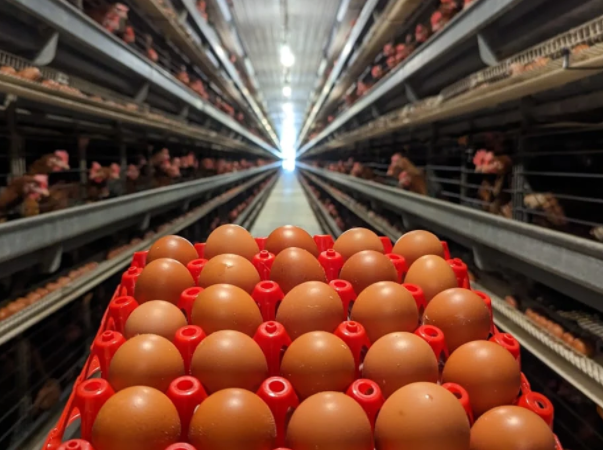
A layer battery cage system can use continuous belts to move eggs toward a central collection point, while an automatic layer cage system coordinates collection timing and transfer.
A published commercial design specifies an 8° cage-floor angle, creating a controlled route from cage to egg belt.
Egg Collection System Parameters
Data is for reference only.Swipe horizontally to view full table.
A type battery cage becomes increasingly valuable when egg volume rises, because an output reference of 12,400 eggs/day requires stable transfer and collection continuity.
Manure Management As A Production Process
Material flow
A type battery cage manure removal should be engineered as a continuous material-transfer process, with belts moving waste from beneath cages toward the house end.
A layer battery cage system can connect horizontal and inclined conveyors to move manure outside the production building.
A reference project uses a manure-pit width of approximately 2.2 m and depth of 350 mm, demonstrating why waste handling must enter the building design stage.
Manure Removal Equipment Parameters
Data is for reference only.Swipe horizontally to view full table.
An Automatic layer cage system can reduce repeated manual waste handling, changing the operation from routine collection to scheduled mechanical transfer.
Automation And Total Operating Cost
Control architecture
A type battery cage automation should match farm scale, production capacity, and maintenance capability rather than adding controls without a defined workflow.
An automatic layer cage system can coordinate feeding, egg collection, manure removal, ventilation, lighting, and environmental monitoring through centralized controls.
A layer battery cage system can therefore shift operator time toward flock observation, inspection, maintenance, and production management.
Automation Module Parameters
Data is for reference only.Swipe horizontally to view full table.
Automation selection should follow the operating scale, because A type battery cage equipment requires coordinated electrical, mechanical, and environmental interfaces for stable operation.
Which System Fits The Farm Business Model?
Project decision matrix
The decision should begin with the target market and housing specification.
If cage-free certification or retailer requirements apply, the project must adopt the corresponding housing architecture.
If conventional commercial production requires controlled egg flow and mechanized manure handling, A type battery cage equipment provides a structured production platform.
Commercial Equipment Selection Parameters
Data is for reference only.Swipe horizontally to view full table.
A type battery cage selection should connect production targets with building dimensions, flock capacity, automation level, and operating conditions.
Our engineering scope can integrate A type battery cage units with feeding, nipple drinking, egg collection, manure removal, ventilation, lighting, and environmental control.
For projects targeting 10,000–30,000 layers, a layer battery cage system can be configured around building dimensions, equipment arrangement, automation requirements, and local production conditions.
Frequently Asked Questions
Q1: What makes A type battery cage economically different from cage-free housing?
A1: A type battery cage concentrates production equipment within defined rows, while cage-free housing allocates additional areas for nests, perches, litter, and bird movement.
A practical comparison should include building utilization, labor organization, equipment investment, and market requirements rather than equipment purchase price alone.
Q2: Can an automatic layer cage system reduce manual work?
A2: Yes.
An automatic layer cage system can mechanize feeding, egg collection, and manure transfer, while plc control coordinates multiple operating functions.
A commercial configuration may use 0.75–1.50 kw feeder drives depending on line design.
Q3: How should a layer battery cage system be selected for a new farm?
A3: Start with flock capacity, house dimensions, local standards, target egg market, and required automation level.
A layer battery cage system should then be engineered around equipment spacing, electrical capacity, ventilation interfaces, manure handling, and future expansion requirements.
Taiyu (HK) Group - One Of China Toppest A Type Battery Cage Manufacturer
A type battery cage provides structured commercial layer housing with four-tier configurations and integrated feeding, drinking, egg collection, and manure-management interfaces.
Global factory direct supply covers poultry equipment packages, engineered components, production specifications, and project-based equipment configuration.
Turn-key engineering integrates poultry equipment selection, house layout, installation coordination, commissioning, and operational handover for commercial layer projects.
Export project support covers equipment production, technical documentation, installation guidance, spare-parts planning, and after-sales engineering coordination.
Factory-based manufacturing supports scalable poultry equipment procurement for international farms requiring standardized specifications and complete project integration.
Contact Us To Received Your Customized Poultry Farm Plan
Headquarters And Branchs
Hong Kong Headquarter Management Team
Hong Kong Headquarter Taiyu Industrial Group CO., LTD
China Hebei Best Machinery And Equipment CO., LTD
Nigeria Vanke Machinery And Equipment CO., LTD
Tanzania Best Machinery And Equipment CO., LTD
Ethiopia Best Hebei Machinery Manufacturing PLC
Reception /24 WhatsApp NO. : +8618830120193
PRODUCTS RECOMMENDED
 China Branch Manufacture Poultry Farm EquipmentRead More
 Ethiopia Branch Manufacture Poultry Farm EquipmentRead More
 Nigeria Branch Manufacture Poultry Farm EquipmentRead More
 Tanzania Branch Manufacture Poultry Farm EquipmentRead More
 IoT Smart Poultry FarmRead More
 >30,000 Layers Automatic H Type Battery CageRead More
 10,000 - 30,000 Layers Automatic A Type Battery CageRead More
MESSAGE
NEWS
 50,000 - 100,000 chickens/house: poultry farm solution, chicken cage, poultry farm equipment, AI smart managementRead More
 30,000 - 50,000 chickens/house: poultry farm solution, chicken cage, poultry farm equipment, AI smart managementRead More
 10,000 - 30,000 chickens/house: poultry farm solution, chicken cage, poultry farm equipment, AI smart managementRead More
 100 - 10,000 chickens/house: poultry farm solution, chicken cage, poultry farm equipment, AI smart managementRead More